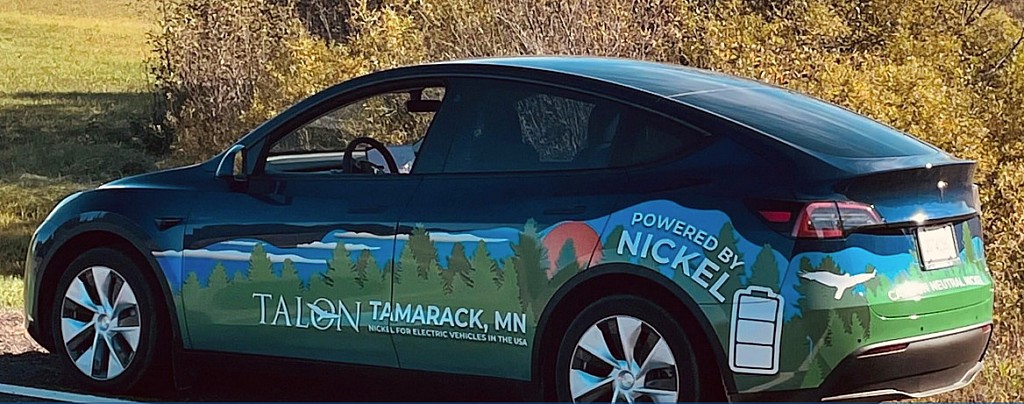

Tesla nickel partner Talon Metals announced on Wednesday it has purchased three additional drill rigs to accelerate battery mineral exploration at its Tamarack nickel-copper-cobalt project mine in Central Minnesota.
Talon said the new drills will be deployed to expand the company’s “exploration of the Tamarack Intrusive Complex for additional high-grade nickel, copper, and cobalt.”
“The need to secure domestic sources of battery minerals like nickel has grown more urgent. Climate change is accelerating, and the United States is dependent on foreign countries for the key ingredients required for clean power and battery storage,” CEO of Talon Metals Henri van Rooyen said. “President Biden, with bipartisan support in Congress, has recently elevated domestic sourcing of battery materials like nickel to a national priority. Our investment in new equipment, people, and technology to explore for battery minerals in Minnesota addresses this national priority and purpose.”
The new rigs will be used to explore additional zones outside of the Tamarack mine’s main resource area. The main resource area is where numerous intercepts of high-grade materials, such as nickel-copper mineralization, have already been discovered, the company said. The mineralization offers up to 9.95 percent nickel.
Talon signed a nickel supply deal with Tesla in January. The exact terms of the deal were unknown, but Tesla did secure 75,000 tonnes of nickel over six years from Talon, who would also provide cobalt and iron ore to the electric automaker for its EV batteries. Additionally, the agreement may be extended “for up to 12 months following which Tesla has a right to terminate the agreement and Talon may elect to sell to other parties.”
Tesla CEO Elon Musk made a call for nickel mining to increase during an Earnings Call in July 2020. “Well, I’d just like to reemphasize, any mining companies out there, please mine more nickel, OK?” Musk asked. “Wherever you are in the world, please mine more nickel, and don’t wait for nickel to go back to some long–some high point that you experienced some five years ago or whatever. Go for efficiency, as environmentally friendly, nickel mining at high volume. Tesla will give you a giant contract for a long period of time if you mine nickel efficiently and in an environmentally sensitive way. So hopefully, this message goes out to all mining companies.”
Tesla also signed an agreement with BHP, an Australian nickel company, in July 2021.
Nickel experts are calling for more domestic production of the material as prices spiked due to the Russian invasion of Ukraine. Trent Mell, a nickel mining expert, told Teslarati in an interview last month that automotive industry leaders, like Musk and Ford CEO Jim Farley, needed to push for more North American production of EV battery materials. Mell’s wishes were answered, as President Joe Biden invoked the Defense Production Act to decrease foreign dependence on materials.
“I am encouraged by this latest measure and what it could mean for the Idaho Cobalt Belt,” Mell said to Teslarati in an emailed statement. “We cannot achieve a low carbon future without new nickel, cobalt, and lithium mines. Building mines in America is important for our national security and industrial interests, and we can realize our clean energy ambitions in a safer, cleaner, and more responsible manner.”
I’d love to hear from you! f you have any comments, concerns, or questions, please email me at joey@teslarati.com. You can also reach me on Twitter @KlenderJoey, or if you have news tips, you can email us at tips@teslarati.com.

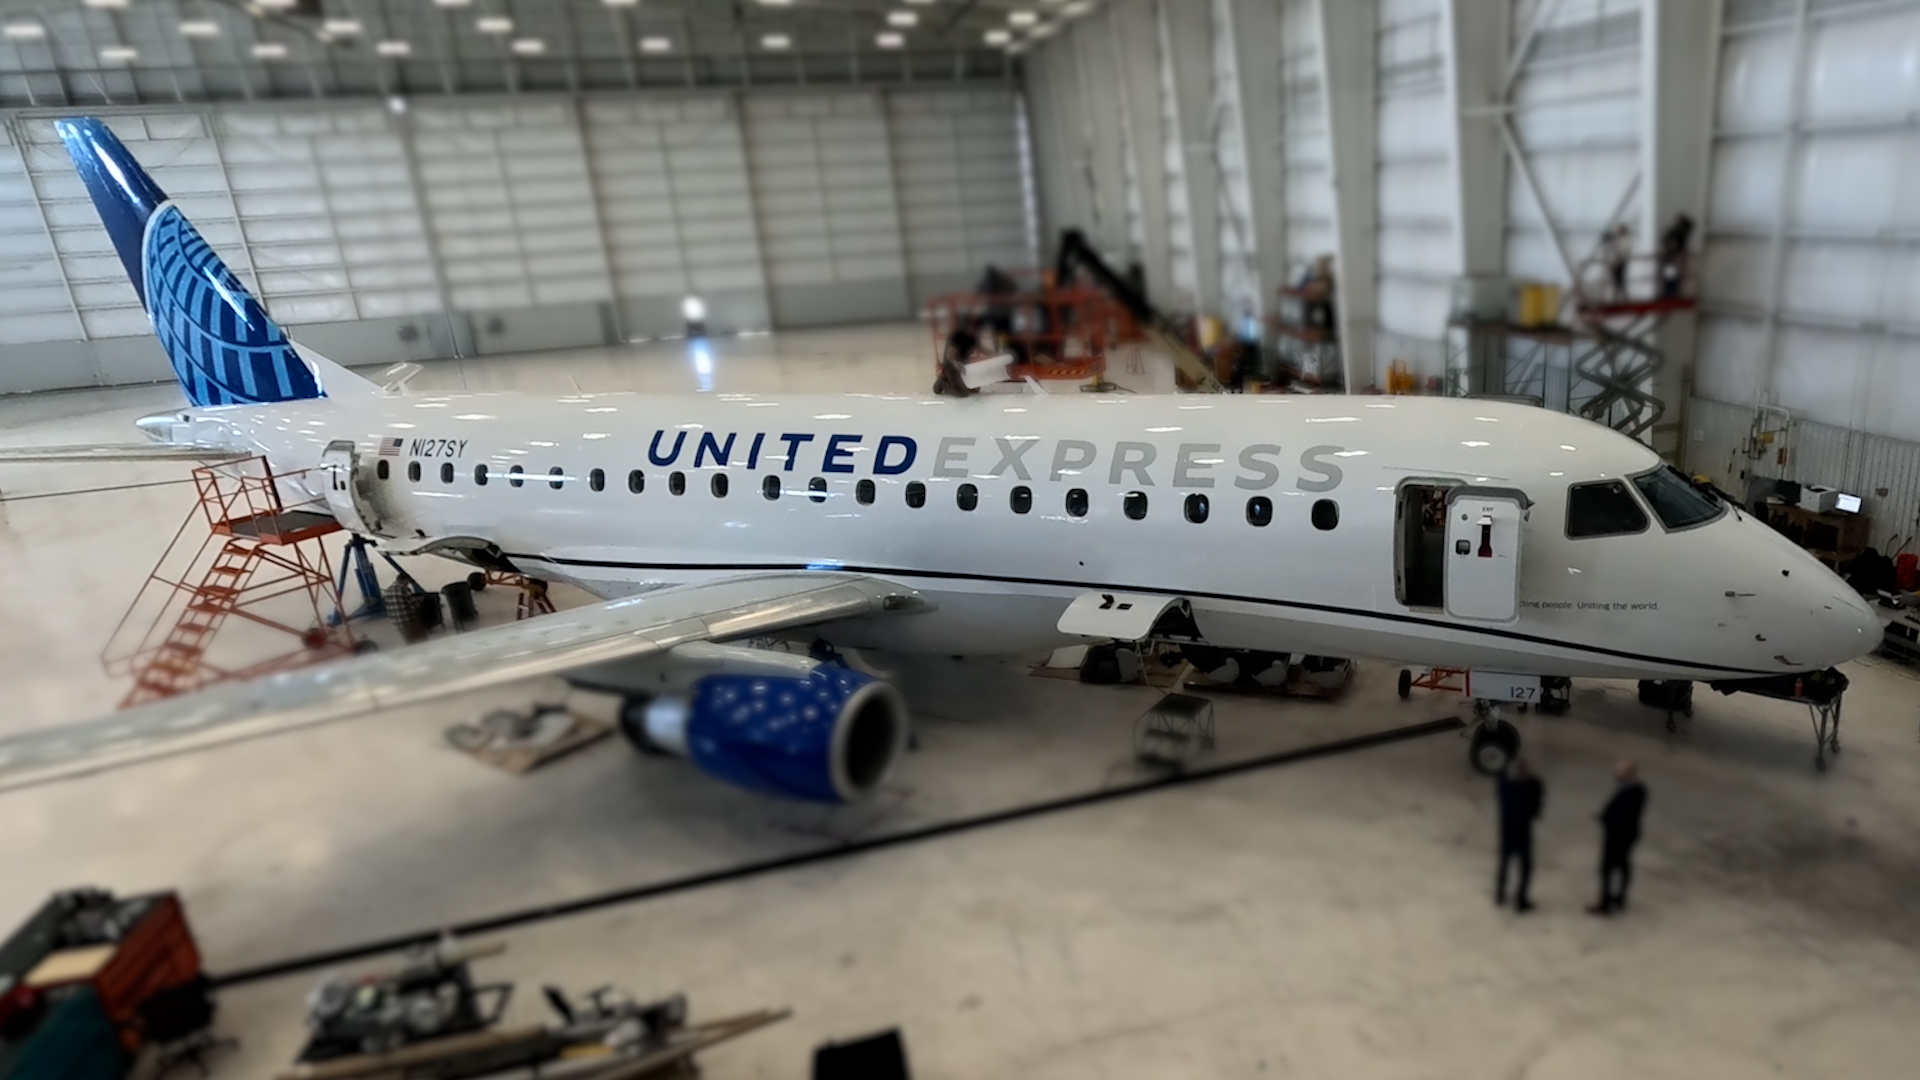
United Airlines CEO Scott Kirby said that SpaceX’s Starlink satellite internet is its leading competitive advantage in the U.S. airline industry. However, in recent comments, while he described the service as “the biggest competitive advantage” the carrier currently holds, he also acknowledged that the edge is temporary.
“…everybody eventually is going to have high-speed low earth orbit internet connectivity. It’s going to be a must-have. We are going to have a few years of being the only airline that has it at scale, and that’s our mission,” Kirby said. Until everyone has it, United aims to capitalize on its head start by converting trial users into long-term loyal customers.
🚨 United CEO Scott Kirby calls Starlink “the biggest competitive advantage,” but says it’s temporary.
“I think it’s the biggest competitive advantage. And it’s temporary. Like it’s not, everybody eventually is going to have high speed low earth orbit internet connectivity. It’s going to be a must-have. But we are going to have a few years of being the only airline that has it at scale, and that’s our mission.”
“I think we’re going to convince customers that United is the best airline and we’re going to get customers to switch their loyalty, to get our credit card, switch their loyalty to United. Not because of Starlink. They’re going to try us for Starlink and they’re going to stay with all the other technology, and everything else is better, and the technology in particular is so much better than technology other, and it’s accelerating because we’ve got the right tech stack, and because we’re like, our gap is getting wider and wider with our technology every day.”
Next: LAX becomes United’s first 100% Starlink hub in the first half of next year, and the United app will show your Starlink odds for each flight. https://t.co/hToyFWaWj7
— TESLARATI (@Teslarati) October 27, 2026
United has moved faster than its rivals on Starlink installations. As of mid-to-late October 2026, the system was on roughly 43 percent of its fleet, with plans to reach 61 percent by year-end, 87 percent by June 2027, and full fleet coverage by the end of next year.
The airline already operates more Starlink-equipped flights than the rest of the U.S. industry combined. Los Angeles International Airport is scheduled to become United’s first 100 percent Starlink hub in the first half of 2027, and the carrier’s app will display the likelihood that any given flight has the service.
Kirby has pointed to early evidence that the offering influences booking decisions. Some passengers loyal to other airlines are already switching flights for Starlink connectivity, something the airline, along with American Airlines, has tried to leverage against competing airlines. Both companies used status-match programs, and some of those customers are pursuing company-specific credit cards, which signals an intent to stay.
Once onboard, these customers encounter the airline’s broader investments in aircraft, larger seat-back screens, oversized bins, connection tools, and a mobile app that Kirby says outperforms competitors. Wi-Fi satisfaction scores on Starlink-equipped planes have been reported to be nearly double those on aircraft with other systems.
Competitors are moving slowly to do the same. Southwest Airlines began installations in 2025 and expects to complete them soon. Delta is pursuing Amazon’s Leo system, while American expects to start Starlink work in early 2027 and has not yet detailed regional-fleet plans. This timeline gap gives United a multi-year window in which it remains the only major U.S. carrier offering Starlink at scale.
Kirby has framed the strategy as pressing that advantage while simultaneously widening gaps in other technology areas so that customers who try United for the Wi-Fi remain for the overall experience.
The approach reflects a calculated bet that superior in-flight connectivity can accelerate share gains and support longer-term financial targets, including a 10 percent pre-tax margin goal.
High-speed internet is particularly valued by premium and business travelers who can work or stream reliably. As low-Earth-orbit service becomes ubiquitous, the temporary nature of the pure connectivity edge means United’s retention will depend on whether its other product and operational improvements keep pace.
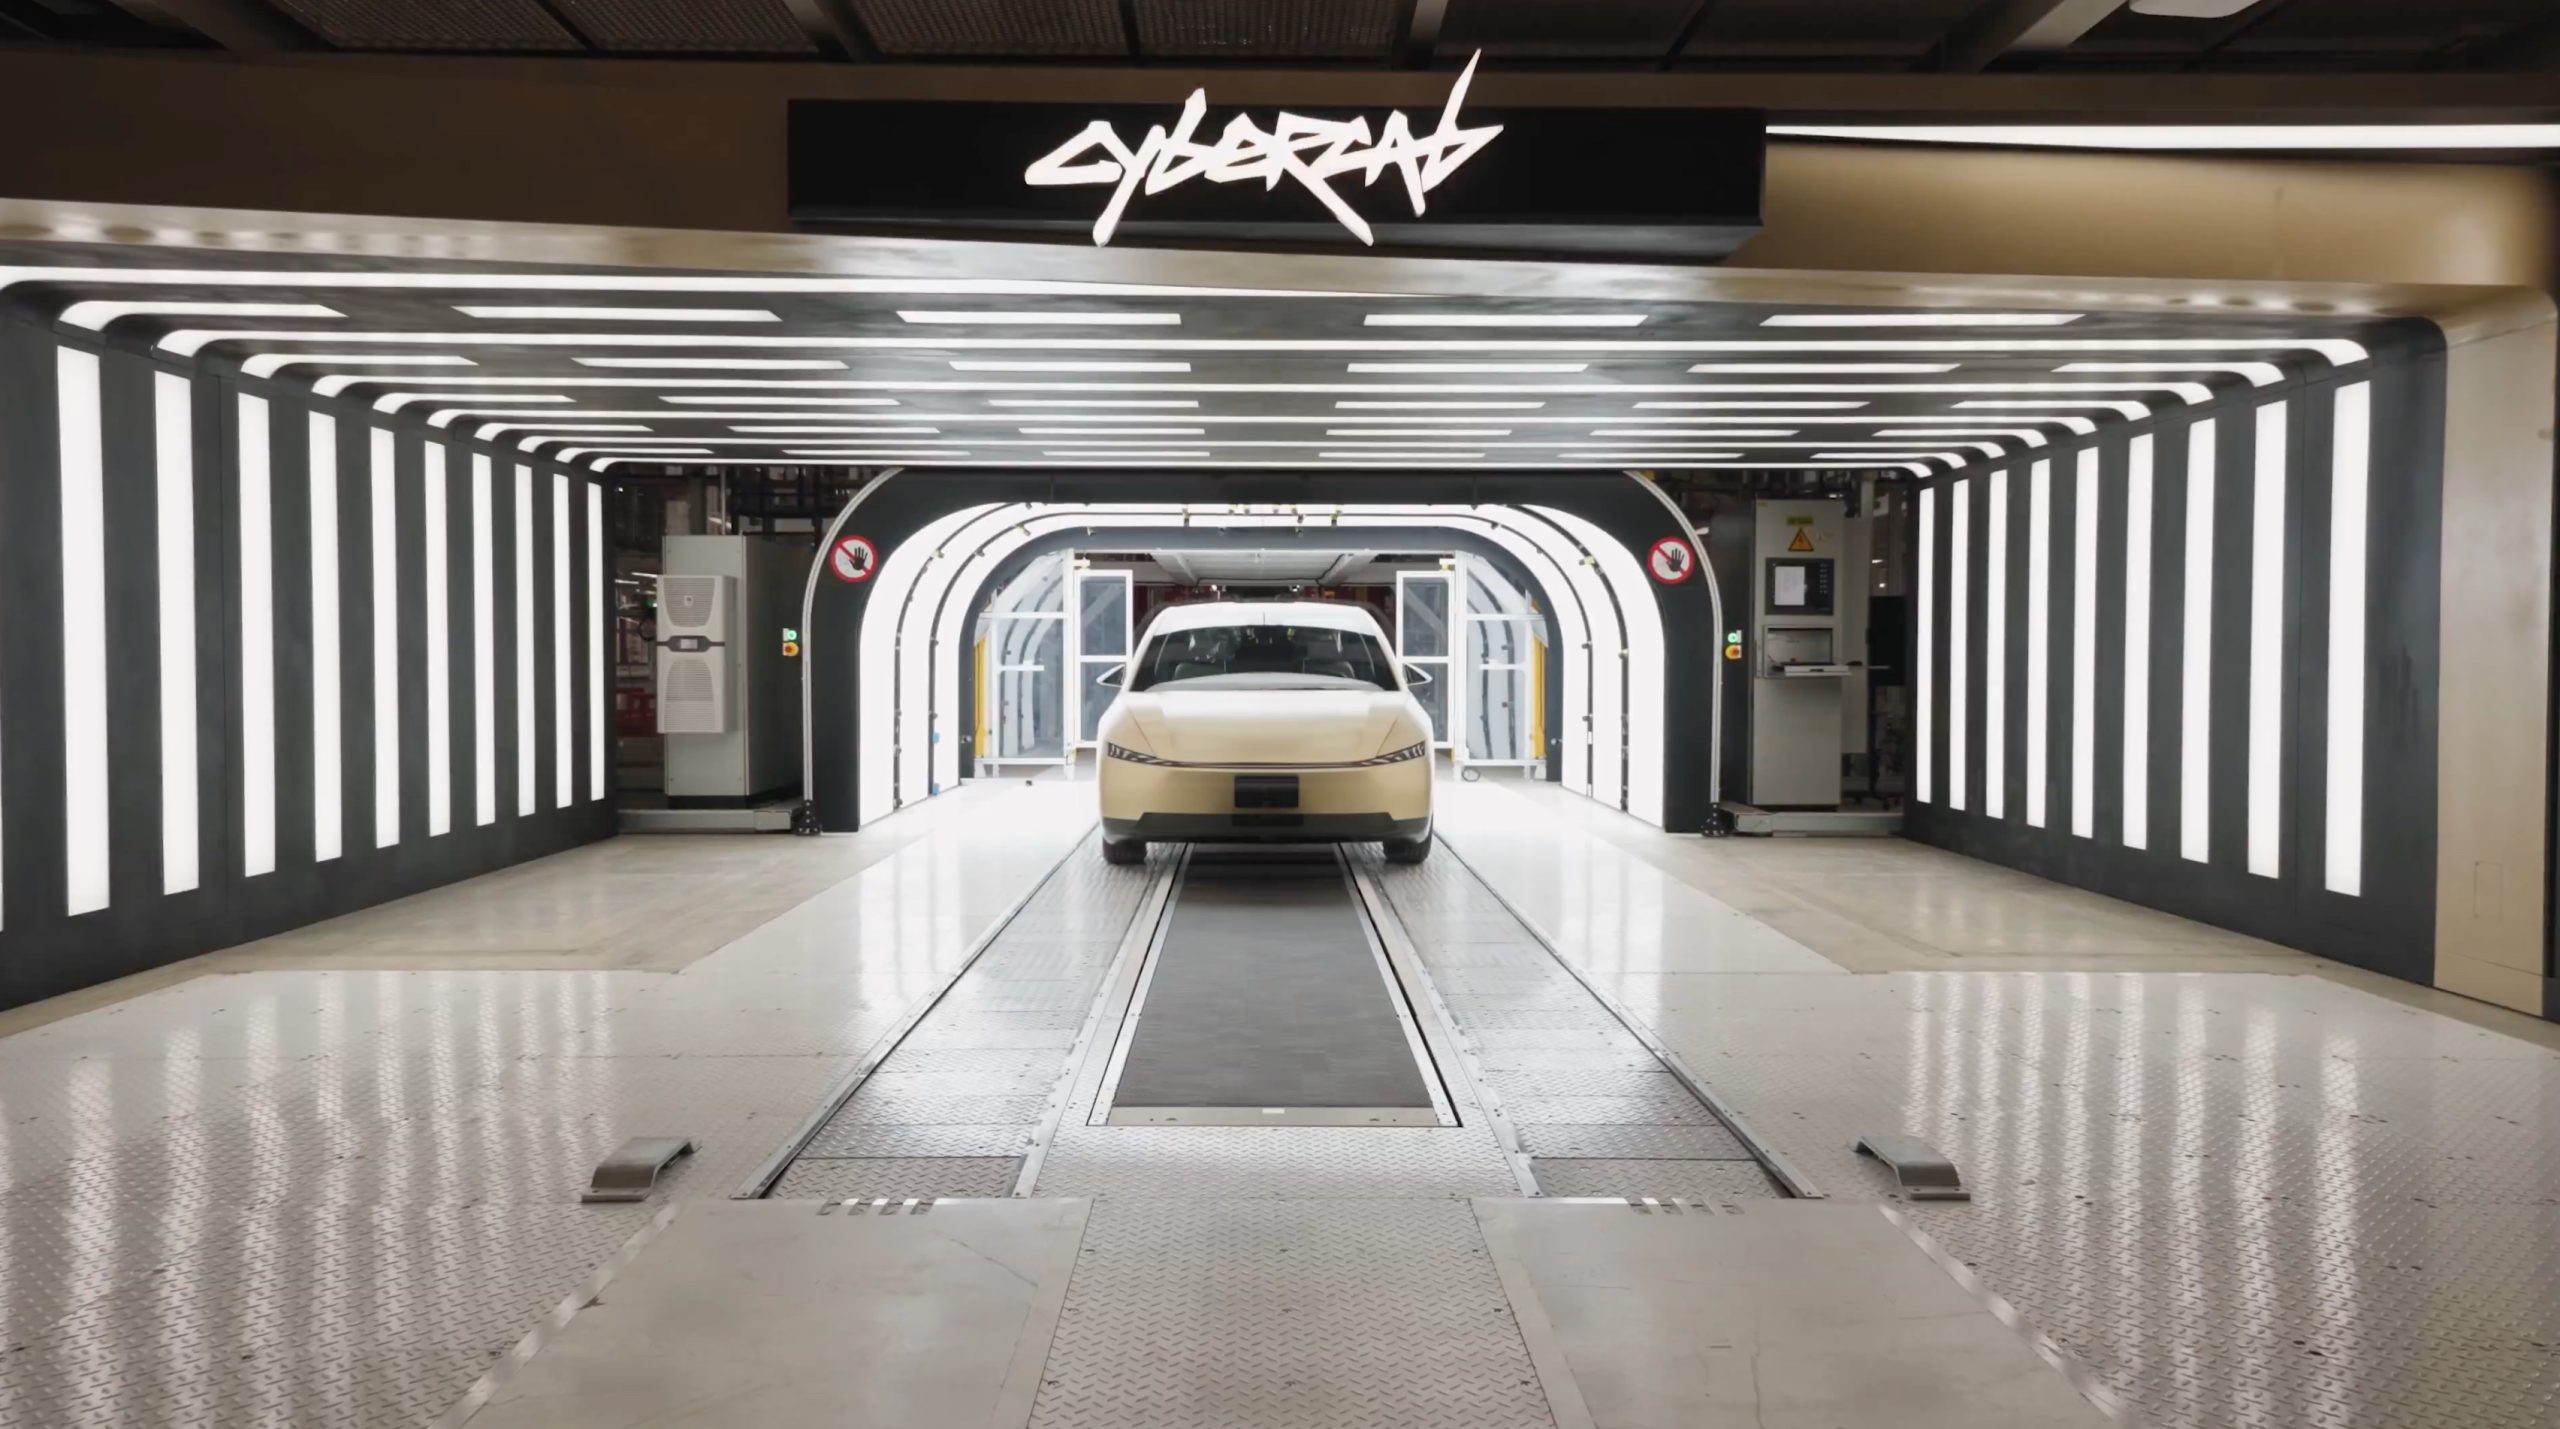
Tesla Cybercab skips the traditional paint shop entirely, marking an unorthodox process for coloring the fully autonomous vehicle. However, the decision was a smart one, as it slashed factory costs, floor space utilization, and complexity, since Tesla relied on specialized alloys and in-mold coloring.
Munro Live was given the opportunity to do a factory walkthrough with Tesla Vice President of Vehicle Engineering Lars Moravy, who explained and detailed how Cybercab production at Giga Texas eliminates one of the automotive manufacturing industry’s most expensive and space-hungry elements.
A conventional paint line can cost hundreds of millions of dollars and require a million man-hours to build. Moravy framed the choice around Tesla’s core rule: “Question the requirements: why do you need paint?”
🚨 Super cool quote from the Cybercab breakdown on the decision to avoid traditional paint:
“One of the most expensive parts of the factory is a paint line… a few hundred million dollars, a million man hours to build one… rule number one at Tesla, question the requirements. Why do you need paint?… the alloys we use in the castings… don’t oxidize and reduce strength over time.” -@larsmoravy
Model Y and Cybertruck bodies are fully coated and painted. On Cybercab, only the side pieces get the anti-corrosion dip coat, and there’s no paint shop at all, which helps cut factory floor space per car by about 50%.
— TESLARATI (@Teslarati) October 26, 2026
The structural answer lies in material selection. The aluminum alloys used in Cybercab’s front and rear castings do not oxidize and lose strength over time, the way many common automotive aluminum alloys do. Only the side modules, built around hot-stamped boron-steel door rings, receive an anti-corrosion e-coat, or dip coat. Front and rear modules skip coating altogether.
Model Y and Model 3 bodies, by contrast, are fully coated and painted.
Exterior colors come from the plastics shop, which Tesla engineers described as “our paint shop” for the Cybercab. Body panels are produced via reaction injection molding, referred to as RIM. Color is then mixed into a polyurethane resin at the mix head immediately before injection, so the panel emerges already colored with a Class-A surface.
Robots trim overflow to control sink marks and flow lines. The process avoids conventional spray-paint defects like orange peel and paint bleed. Scratches can still be repaired with compatible coatings that behave “basically like paint.” Because color is integral rather than a surface layer, shallow scratches do not expose a contrasting undercoat.
The secret behind Tesla’s Cybercab Gold goes well beyond just the color
Tesla has also explored related approaches, including in-mold lamination and painted films on stamped panels.
The manufacturing payoff is substantial because removing the paint shop, combined with the “unboxed” modular process that builds and tests front, rear, side, and center modules in parallel before a short final assembly, cuts factory floor space per vehicle by about 50 percent.
Final assembly itself uses only about 25 automated stations, far fewer than the typical Model Y line, and the overall line runs at about 78 percent automation, Moravy said. The approach also eliminates volatile organic compound emissions associated with traditional spray painting for these panels and shortens the coloring cycle from hours to minutes.
Cybercab’s paint strategy is clearly less about aesthetics than about systematically deleting capital-intensive, energy-heavy, and space-consuming steps once material science and process design make them unnecessary. It is a concrete example of Tesla applying first-principles questioning to one of the auto industry’s most entrenched factory requirements.
Investor's Corner
Tesla has a Cybercab problem nobody saw coming
Tesla’s Cybercab line now builds robotaxis faster than Tesla can deploy them, Lars Moravy says.

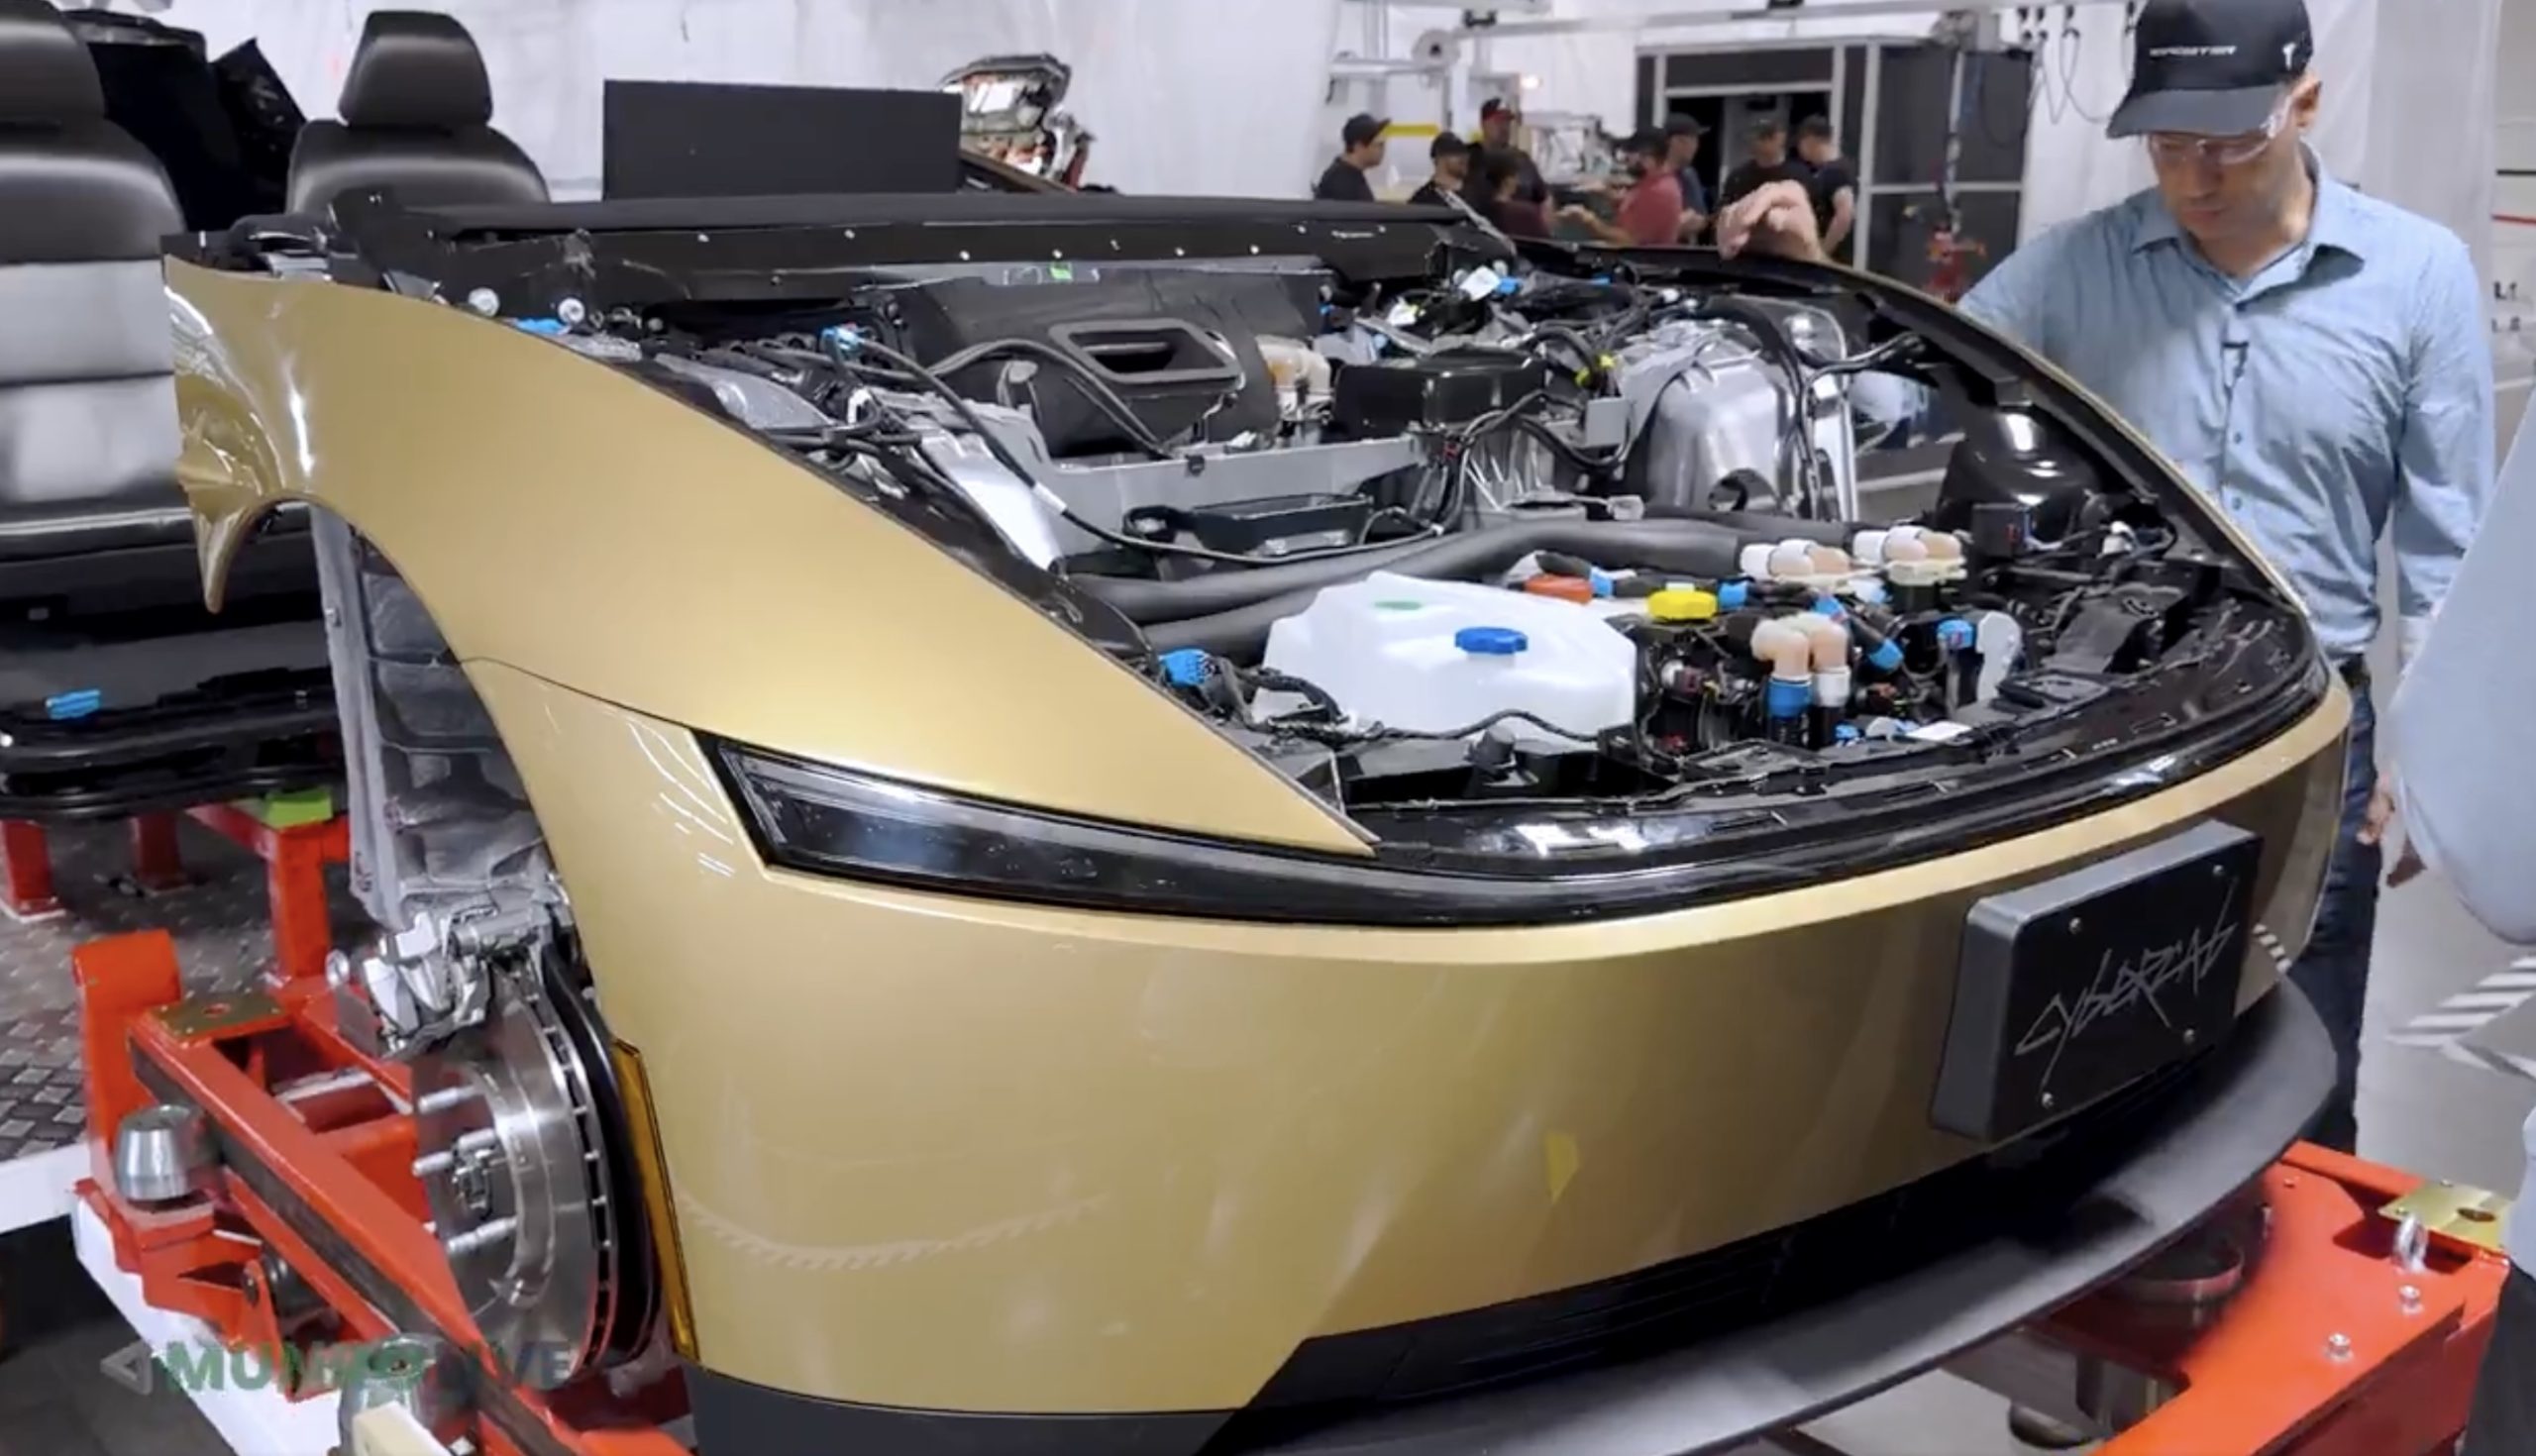
Tesla’s Cybercab line in Texas can now build the two seat robotaxi faster than the company can put it into service, according to Lars Moravy, Tesla’s Vice President of Vehicle Engineering. “We don’t run every day because the line can run so fast. It’s currently outpacing our deployments,” Moravy said in a new Cybercab deep dive from Munro Live. “So, it’s a bit of a race right now. Who’s going to go faster? Right now the manufacturing line’s ahead.”
Tesla’s official Robotaxi account shared a Cybercab analysis video on X on Monday, calling it a “Cybercab engineering deep dive.” Moravy’s comments go further than what he told analysts on the Q3 earnings call last week, when he said the Cybercab line’s listed capacity of more than 125,000 units a year undersells what it can actually run.
The tour shows where that speed comes from. Tesla’s unboxed process splits the Cybercab into front, rear, side and center modules that are built and tested on their own before they meet on a short final line. That final line has just 25 fully automated stations, which Tesla’s team estimated is a fifth to a tenth of what a Model Y needs. The full line is about 78% automated, the framing line is already at 100%, and the layout uses roughly 50% less floor space per vehicle. The stated goal is “100% automation in 10 second cycle time,” or one finished Cybercab every 10 seconds.
Tesla also deleted the paint shop. Only the side modules are coated, and the exterior panels get their color inside the molding machine. Engineers said the car is designed to run at least 500,000 miles, which matters for a vehicle that will spend most of its day carrying riders.
The battery got the same treatment. The Cybercab uses an 88S6P pack of 4680 cells in a steel enclosure, a first for Tesla, with each module potted separately so a single failed module can be swapped instead of the whole pack. Wireless battery management boards replace a wiring harness, and new contactors are fast enough to drop the pyro fuse entirely. Tesla’s battery director graded the pack an A minus, compared with a D for the Model Y structural pack and a B minus for Cybertruck. Up front, the drive unit runs an 11:1 gear ratio versus roughly 9:1 on most Teslas, since the Cybercab does not need a high top speed.
Cybercab engineering deep dive — Robotaxi (@robotaxi) October 26, 2026
The deployment side is now the bottleneck Moravy described. Tesla had more than 50 Cybercabs working the Formula 1 weekend in Austin, and Texas records show 463 Cybercabs registered. Tesla said on its earnings call that Cybercab service will launch in Dallas next month, and Moravy said the company is aiming to get Cybercabs to customers by the end of 2026. Every unit built so far has gone into Tesla’s own fleet since the line moved into volume production in April.
Munro Live also asked when it could get a Cybercab to tear down. Tesla’s answer: “Not yet.”

Starlink is ‘biggest competitive advantage,’ but it’s temporary, United CEO says

Tesla Cybercab’s unorthodox paint process explained


